CNC TECHNICAL GUIDE
CNC Router for Aluminum: What Actually Matters?
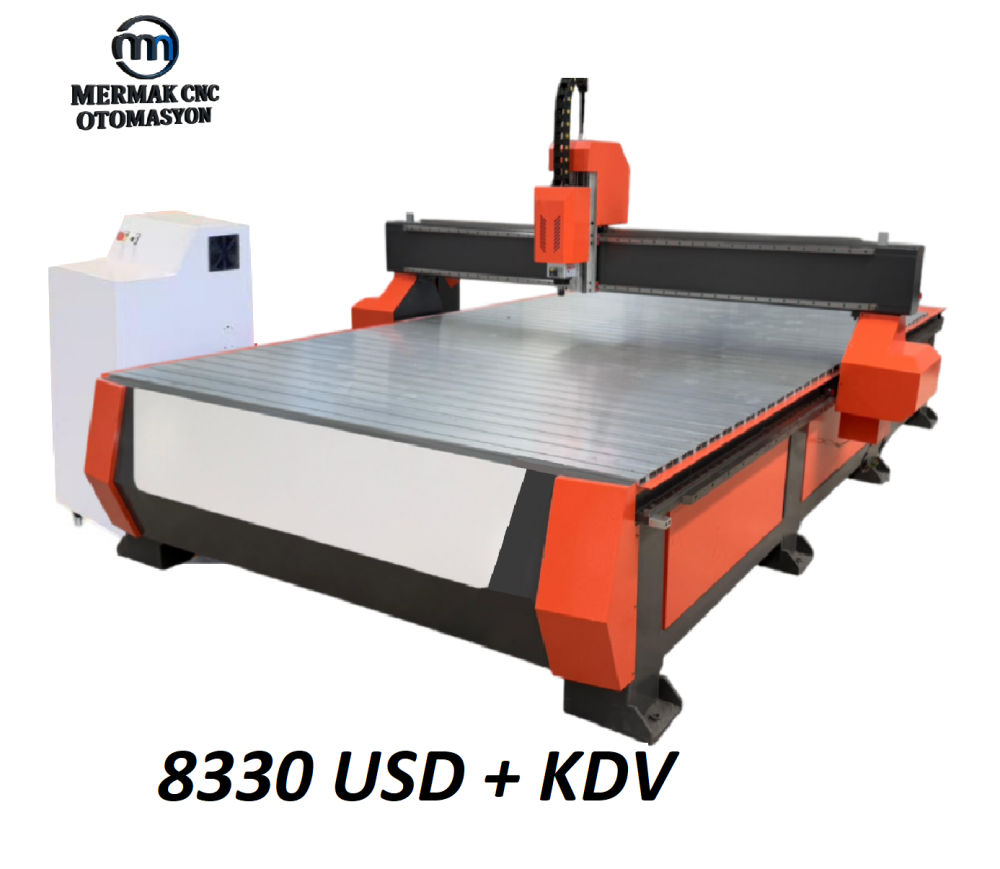
Many CNC routers can machine aluminum, but good results depend on much more than whether the spindle can spin a carbide end mill. Rigidity, chip evacuation, workholding and the cutting strategy decide whether the process is productive.
Rigidity first
Aluminum cutting forces can excite vibration in a flexible frame or gantry. Excessive deflection shows up as chatter, poor finish, dimensional error and shortened tool life.
Spindle speed and chip load
Running maximum RPM is not automatically correct. Feed rate, number of flutes and RPM determine chip load. Cutting too slowly for the selected RPM can rub instead of cut.
Use suitable tooling
Sharp carbide tools designed for non-ferrous materials help evacuate chips. Single- or two-flute tools are common on routers because they create more chip space.
Keep chips away from the cutter
Re-cutting hot chips rapidly damages surface finish and tool life. Air blast, extraction and appropriate lubrication or mist strategies can improve process stability.
Workholding must be rigid
Thin aluminum can vibrate even on a rigid machine. Fixtures, clamps or vacuum systems must prevent the sheet from lifting or moving.
Start with conservative engagement
Use shallow radial engagement or suitable adaptive strategies when testing a new setup. Measure spindle load, listen for chatter and inspect the chips.